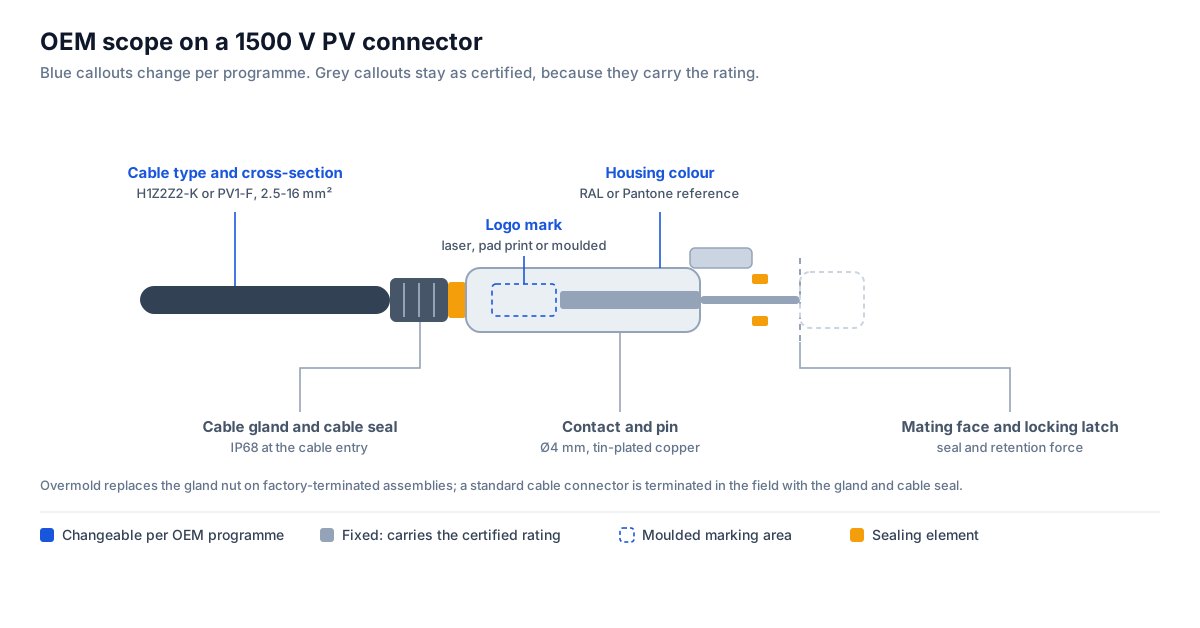
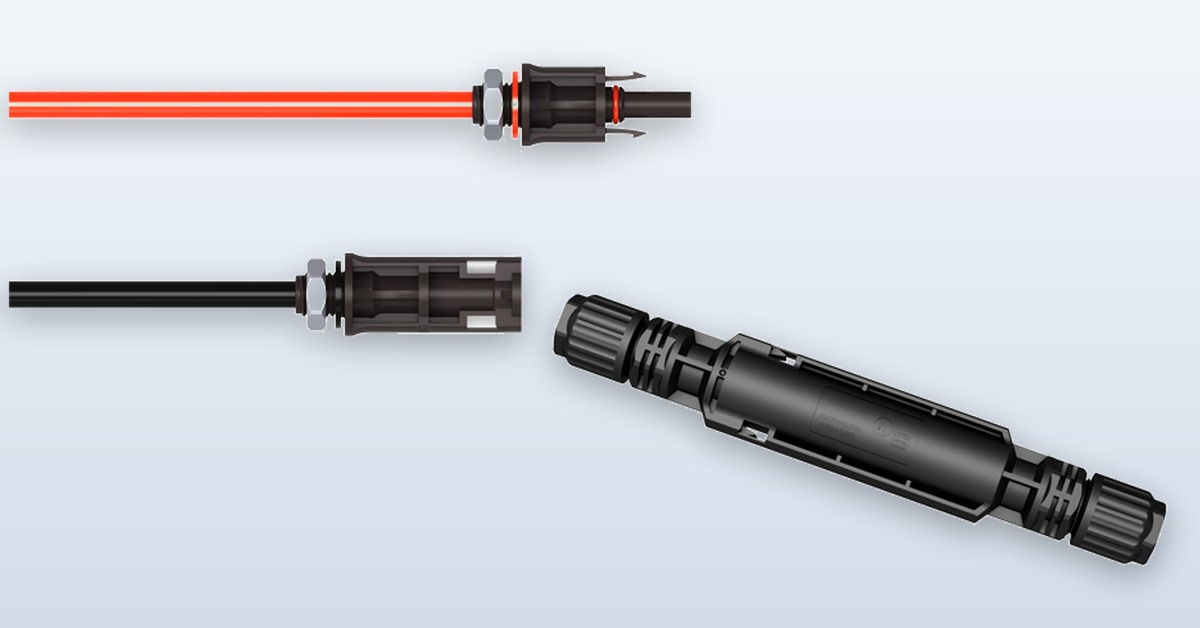
A 1500 V MC4 connector OEM programme splits into two halves. Housing colour, logo mark, cable type and overmold geometry are built to your drawing. The contact, the sealing and the locking geometry stay as certified, because those parts carry the 1500 V rating. Treasol is an independent manufacturer in Dongguan and is not affiliated with Stäubli, the owner of the MC4 trademark.
The split below is the one that matters commercially: changing the parts on the left is a tooling and artwork question, changing the parts on the right is a re-test question. Programmes that stay on the left move quickly. Programmes that touch the right side need a test plan before a sample is built.
Both models below are rated 1500 V by TÜV Rheinland and UL and share the 4 mm mating geometry, so a cable connector and a panel connector built to the same programme mate with each other. Values are the published product data.
| Parameter | CN4U-C cable connector | CN4U-P panel connector |
|---|---|---|
| Rated voltage | 1500 V (TÜV), 1500 V (UL) | 1500 V (TÜV), 1500 V (UL) |
| Rated current | 70 A max | 52 A max |
| Test voltage | 12 kV (TÜV, 50 Hz, 1 min) | 12 kV (TÜV, 50 Hz, 1 min) |
| Contact resistance | below 0.5 mΩ | below 0.5 mΩ |
| Degree of protection | IP68 | IP68 |
| Ambient temperature range | -40 °C to +85 °C | -40 °C to +85 °C |
| Insulation material | PPE / PA66 | PPE / PA66 |
| Contact material | Copper, tin plated | Copper, tin plated |
| Flame class | UL 94 V-0 | UL 94 V-0 |
| Safety class | II | II |
| Pin dimensions | 4 mm | 4 mm |
| Conductor cross-section | 2.5 / 4.0 / 6.0 / 10 / 16 mm² (14-6 AWG) | 2.5 / 4.0 / 6.0 mm² (14-10 AWG) |
Full dimensions, derating curves and the applicable certificate per model are in the CN4U-C and CN4U-P product data, and in the datasheet library.
"MC4-compatible" describes the 4 mm mating geometry: the plug and socket fit each other and latch. It is a dimensional statement, not a certified one. It does not say that a connector from one manufacturer and a connector from another have been tested together, and it does not transfer a certificate from one product to another.
In the United States the point is written into the code rather than left to interpretation. NEC 690.33(C) requires mating connectors to be of the same type and from the same manufacturer, or to be documented as compatible by both manufacturers. Where a mixed pair is unavoidable, the documentation has to exist before the installation, not after a fault. Our cross-mating guide sets out the same boundary in more detail.
Trademark and independence. MC4 is a registered trademark of Stäubli Electrical Connectors. Treasol is an independent manufacturer of PV connectors and is not affiliated with, authorised by or endorsed by Stäubli. We do not claim that our connectors are identical to, or interchangeable in every respect with, Stäubli products.
What we do not write. We do not describe any connector as "100% compatible with MC4", and we do not state a compatibility percentage. Where a customer asks for a mixed assembly, we ask for the two part numbers and answer in writing.
The practical test is mechanical fit plus a documented rating. If a programme needs a connector that mates with an installed base, the mating half is specified on the drawing and verified on samples before the run — the same gate as any other dimensional requirement. Details of the geometry are on the MC4-compatible connector page.
Seven gates. Each one produces something the customer signs before the next one starts, so the schedule is not a guess and the sample is not a hand-made part.
Drawing or target specification, cable type, cross-section, quantity, target market and the standard the assembly has to meet.
Output: RFQ packageFeasibility against the certified design, tolerances, crimp and moulding method, and the test plan for the finished part.
2-3 working daysExisting tool, modified tool or new tool. Cost, lead time and tool ownership are agreed in writing before anything is cut.
Output: tooling planSamples are built on the production line with production tooling, so the sample is representative of the run.
5-7 or 7-12 working daysDimensional check, pull-out force on the crimp, contact resistance and an IP check, reported against the drawing.
Customer sign-offInjection moulding, crimping, assembly and in-process inspection against the released drawing.
15-20 or 20-30 daysPrivate-label packing, carton marks, documents and release to the nominated freight forwarder.
Output: packing list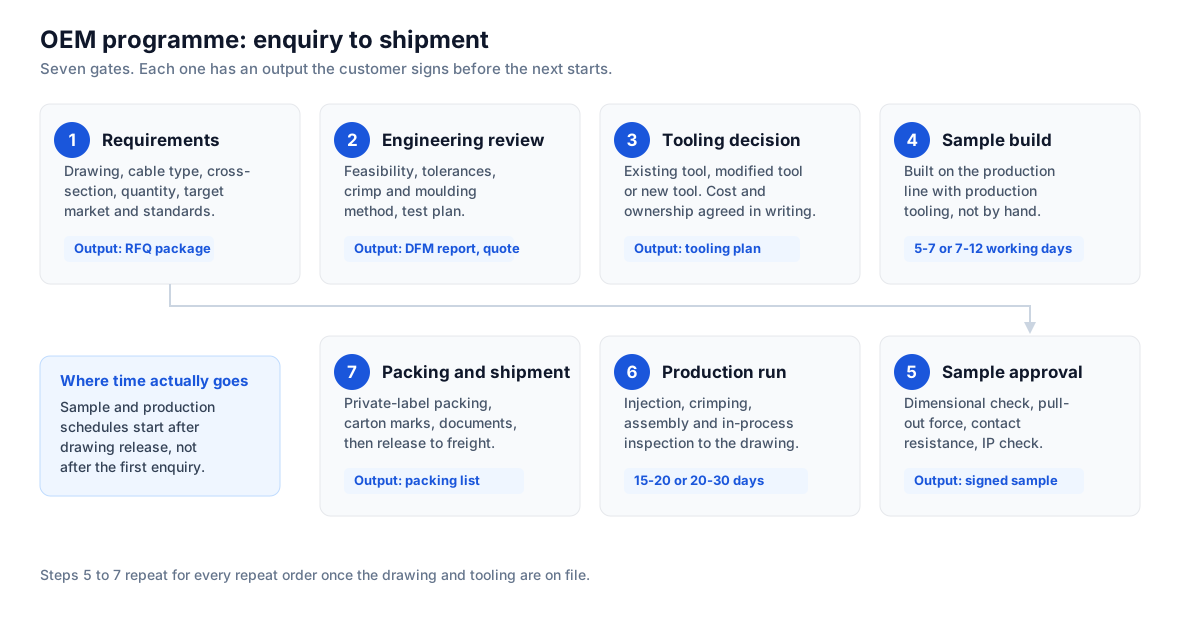
The checks below are the ones run in-house on the equipment shown, on the production line rather than in a separate lab. The full process, including moulding, crimping and assembly, is documented on the PV connector manufacturing page.
| Check | What it establishes | Equipment |
|---|---|---|
| Crimp pull-out force | The crimp holds the conductor under load, with the limit set per cross-section | Pull-out force tester, tensile tester |
| Contact resistance | The joint stays below the published limit at rated current | Programmable DC power supply, milliohm measurement |
| Dielectric withstand | Insulation holds the test voltage without breakdown | Dielectric withstand voltage tester |
| Insertion and withdrawal force | The latch engages and releases within the specified force window | Insertion and withdrawal force tester |
| Ingress protection | The mated pair and the cable entry hold the IP68 rating | IP test rig |
| Damp heat and temperature cycling | The housing and seal survive the service environment | Constant temperature and humidity tester |
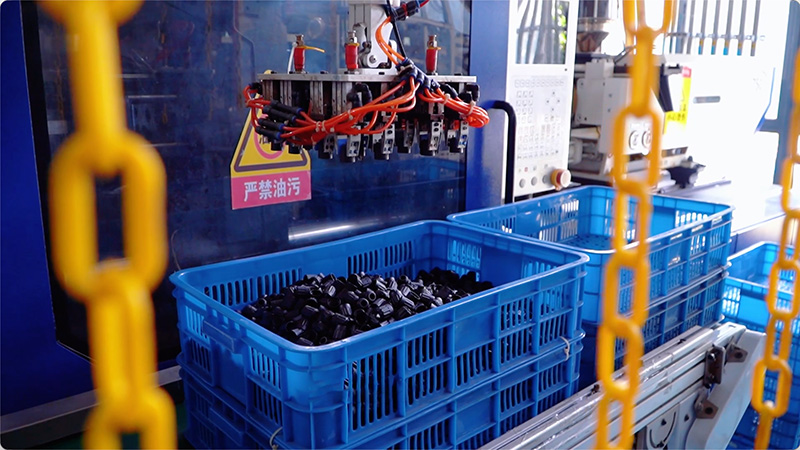
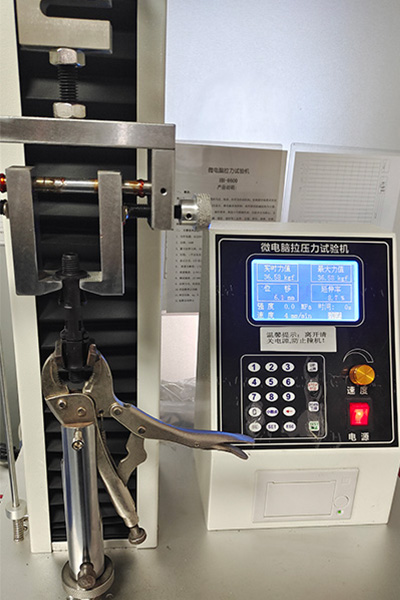
Sampling. Crimp pull-out force and contact resistance are checked at set-up and at defined intervals during a run; visual and dimensional checks run on every assembled set. The exact sampling plan for a programme is written into the inspection document that ships with the order.
Numbers below are the ones we commit to in writing. Where a figure depends on the programme — tooling, quantity, destination — it is confirmed with the quotation rather than estimated here.
| Term | Position |
|---|---|
| MOQ, standard models | No fixed minimum. Standard connector models can be ordered from one piece. |
| MOQ, OEM run | Quoted per programme. Set by whether existing tooling can be used or a new tool has to be built. |
| Samples | 1-5 sets, built before the production run and credited against it. |
| Sample lead time | 5-7 working days for a repeat configuration, 7-12 working days for a new drawing. |
| Production lead time | 15-20 days after drawing release for a repeat configuration, 20-30 days after sample approval where the design is new or needs new overmold tooling. |
| Packaging | Bulk cartons as standard. Private-label bags, printed carton marks, barcodes and labelled bundles are produced to your artwork. |
| Trade terms | Confirmed with the quotation for the destination and order size. |
| Payment terms | Confirmed with the quotation. Tooling and production are billed separately where a new tool is built. |
For buyers who resell rather than build under their own name, the wholesale supply programme for distributors sets out tiered pricing, mixed pallets and the documentation pack. For assemblies rather than loose connectors, the custom PV wire harness line covers branch sets, string extensions and inverter input looms.
Yes. The housing can carry a laser mark, a pad-printed mark or a moulded mark, and the housing colour can be changed to your specification. A marking drawing or artwork file is required before the sample build, and the mark is applied to the production part, not added afterwards.
Standard connector models carry no fixed minimum and can be ordered from one piece. An OEM run with a custom colour, mark, cable or overmold is quoted per programme, because the quantity depends on whether existing tooling can be used or a new tool has to be built.
The rating belongs to the tested construction. Changes to housing colour, marking, cable type and overmold geometry are evaluated against the certified design, and any change that affects the contact, the sealing or the locking geometry goes back through testing. The applicable certificate scope is confirmed per model before the order is released.
The crimp terminal has to be crimped with a tool and die set matched to that terminal and conductor size. We supply or specify the crimping tool, the die and the pull-out force limit for the cross-sections in use, and crimp samples are verified before a production run starts.
A 4 mm contact geometry can mate mechanically, but that is not the same as a certified or permitted combination. NEC 690.33(C) requires that mating connectors be of the same type and from the same manufacturer, or be documented as compatible by both manufacturers. Mixed pairs should be treated as an engineering decision with written confirmation, not as an assumption.
Samples take 5-7 working days for a repeat configuration and 7-12 working days for a new drawing. Production runs 15-20 days after drawing release for a repeat configuration, and 20-30 days after sample approval where the design is new or needs new overmold tooling. Freight and any customer inspection add to the door-to-door time.
Send the drawing or the target specification and the annual band you are planning for. Engineering replies with a feasibility note, the tooling position and a sample schedule.
Send the drawing, the target market and the annual band. We will tell you what can change, what cannot, and what the first article will cost and take.
Contact the OEM team